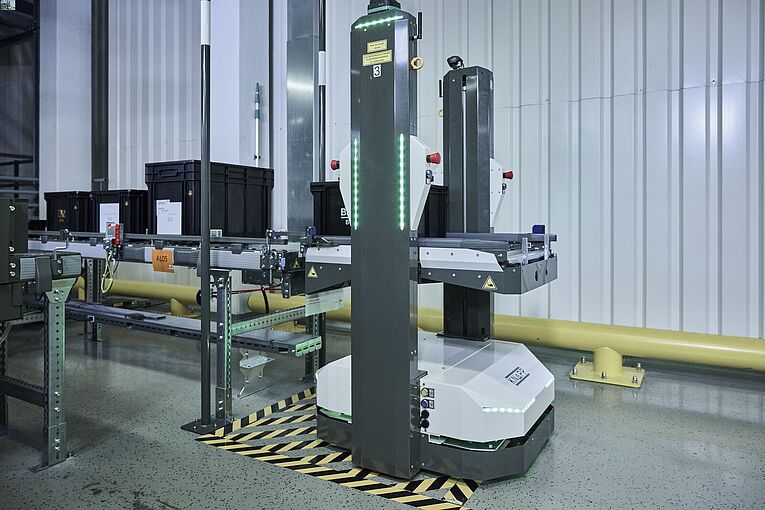
Adaptive manufacturing combines integrated building blocks into a cohesive production architecture. The goal is to design automation in a way that no longer forces trade-offs between speed, flexibility, and regulatory compliance—but optimizes them simultaneously. A key lever is how products move through production. Instead of rigid, sequential lines, systems emerge in which products can move individually, be buffered, and prioritized. Process steps are decoupled, enabling changes to be implemented in software rather than through complex mechanical modifications. This allows for significantly faster changeovers and reduces downtime, especially in environments with frequent product changes and smaller batch sizes.
At the same time, previously separate functions such as control, motion, machine vision, and quality assurance are integrated into a unified automation architecture. This enables real-time synchronization of processes, while quality checks are performed continuously during production. Errors are detected early and can be corrected immediately—an essential advantage in pharmaceutical manufacturing, where quality management is critical to overall efficiency.
Another key component is the end-to-end use of machine simulation and digital twin technologies. Machines and processes can be developed, tested, and optimized virtually before physical implementation. Changes can be validated in advance, risks identified early, and commissioning and requalification efforts significantly reduced—from days to hours.
This flexibility is underpinned by an open and integrated data architecture. Machines, subsystems, and IT systems are connected across all levels, generating continuous data streams. These enable real-time monitoring and predictive analytics, helping to detect and prevent deviations early. At the same time, complete traceability is ensured—a core requirement for regulatory compliance and efficient release processes. Together, these elements form a new production paradigm for Europe’s pharmaceutical industry—one that fundamentally differs from traditional automation concepts. The focus is no longer on maximizing the utilization of fixed lines, but on the ability to continuously adapt to new requirements.
“For ‘Pharma made in Europe’, this means managing increasing complexity while maintaining high levels of efficiency, quality, and compliance. That is where the decisive competitive advantage lies,” says Patsakas.